WHO WE ARE CEYLON BEVERAGE
Ceylon Beverage International (Pvt) Ltd is a leading and trusted beverage manufacturing and contract-filling partner in Sri Lanka. We combine quality, innovation and manufacturing excellence to deliver safe, consistent and refreshing beverage solutions—from processing and filling to packing. Driven by excellence, trusted by partners, and committed to every refreshment we create.
OUR
STORY
Ceylon Beverage International (Pvt) Ltd was born at the heart of Sri Lanka's export hub — the Horana Export Processing Zone at 2020. We were founded with a singular vision: to build the most advanced, internationally compliant beverage manufacturing facility in South Asia.
From that founding, we rapidly scaled to a capacity of 600 million units per year — earning FSSC 22000, ISO 9001, ISO 14001, ISO 45001 and HALAL certifications along the way. Today, over 10 brands across Sri Lanka and global export markets trust CBI to bring their beverage vision to life with precision and care.
MISSION · VISION
AND VALUES
Deliver optimum value to our stakeholders
Deliver optimum value to our stakeholders through beverage processing development, improving the productivity & quality, while creating an open culture within the organization to creativity and innovation to be competitive.
Nation’s leading beverage manufacture
To become the nation’s leading beverage processing & filling solution provider.
Principles That Guide Everything
- Quality Without Compromise
- Innovation & Technology
- Customer Partnership
- Environmental Responsibility
- Integrity & Transparency
- People Development
- Safer Workplace
SCALE THAT DELIVERS
Over 6 years of manufacturing excellence, serving 10+ brands from our state-of-the-art facility in Sri Lanka.
BUILT FOR
SCALE
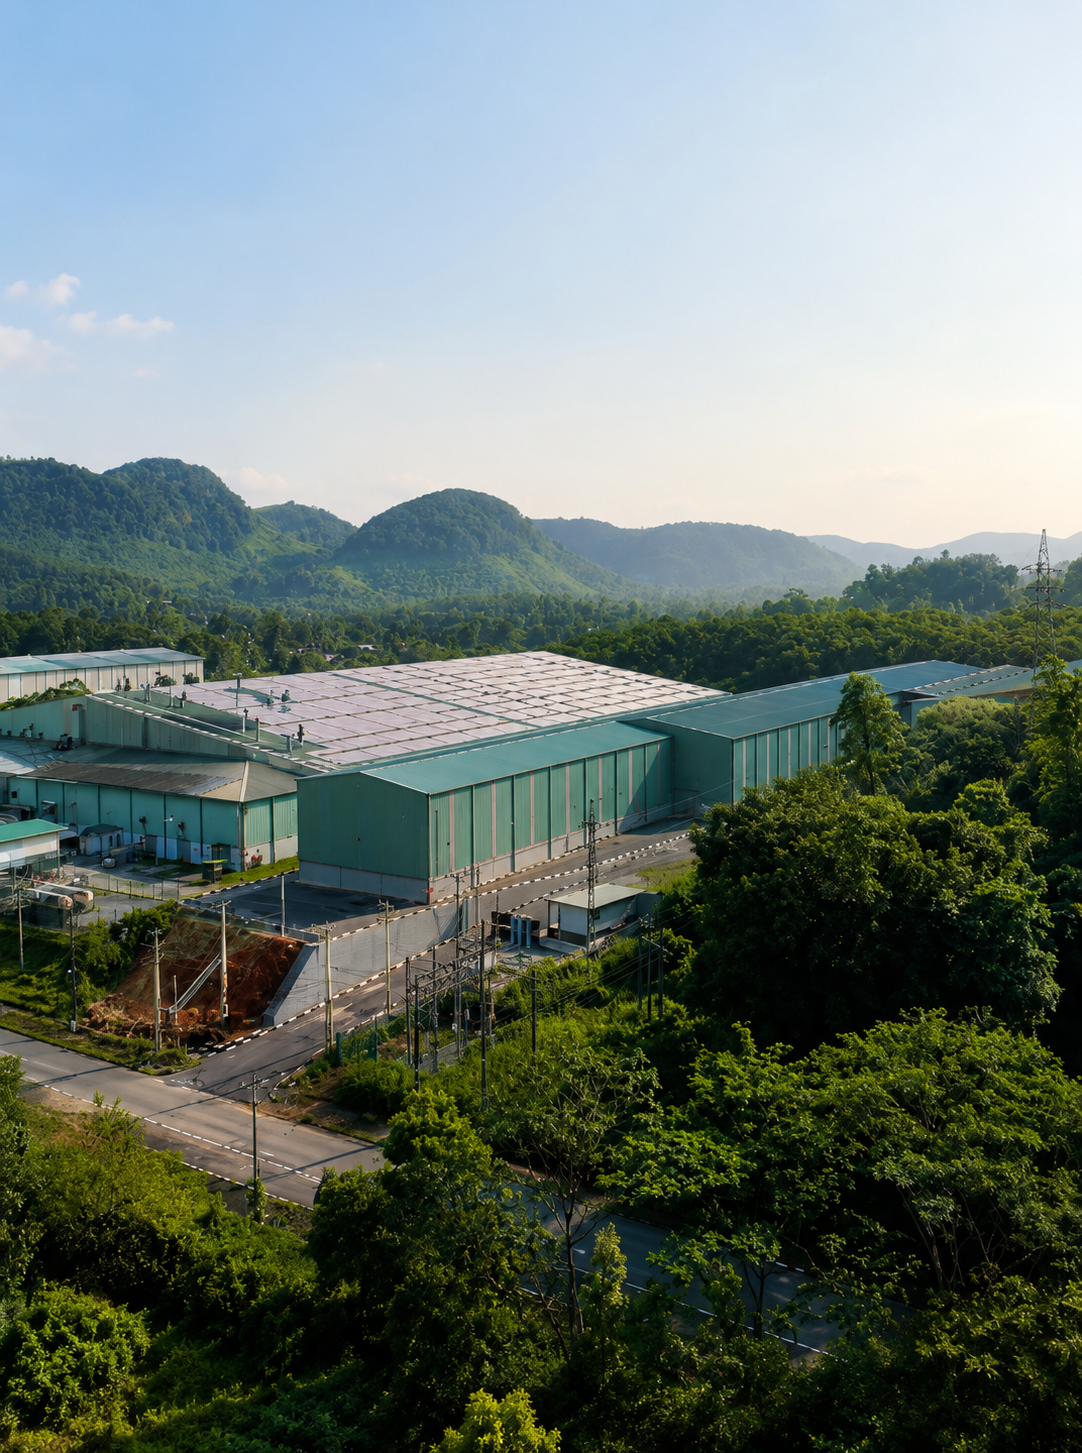
Spanning over 260,000 sq ft within the Horana EPZ, our facility houses state-of-the-art filling lines, a dedicated R&D laboratory, advanced water treatment systems, comprehensive microbiological analysis capabilities, cold chain logistics, extensive finished goods storage facilities, and full ETP compliance. Designed to support everything from small-batch trials to large-scale manufacturing, the facility is equipped to efficiently handle production volumes exceeding 600 million units annually.
See Manufacturing Capabilities
INTERNATIONALLY AND
LOCALLY CERTIFIED
Every product leaving our facility meets the strictest global food safety, quality, and compliance standards.
START YOUR
PROJECT TODAY
From concept to container — we handle R&D, formulation, filling, packaging, and export. Your brand deserves a manufacturer who cares as much as you do.